STAVITRODE A 57
DESCRIPTION & APPLICATIONS :
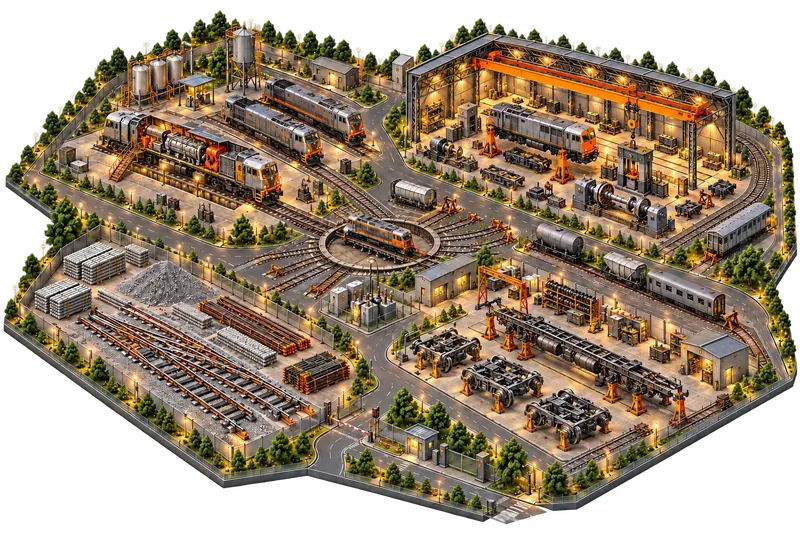
Moly-manganese rutile electrode for general use, depositing tough, hard surfacings that withstand impact. Medium manganese steels are its main target: repair of rail frog and crosspiece, armouring of worn rail surfaces and flanks, plus wear-resistant build-up and overlays.
It is well matched to wear-loaded machine members in unalloyed and low alloyed steels subjected to dragged and crushing loads (worms, toothed gears, gear parts). Machining of the weld metal is possible.
Applications: hammers, wobblers, excavators, pinions, couplings, tail bars, key ways, gear teeth, dozer sprockets, carrier and track rollers, idlers, crane wheels, and rail frogs and crosspieces.
Heat treatment: preheat to suit the base material; for materials prone to cracking, go up to at least 300°C.
UNIQUE FEATURES :
- Moly-manganese deposit for general use, with 36 - 40 HRC without treatment.
- Surfacing is tough, hard and impact resistant.
- Weld metal can be machined.
- Current: AC or DC (+). Re-drying: 1 hour at 100°C.
Product details
KEY SPECIFICATIONS :
| C | Si | Mn | Ni | Cr | Mo |
|---|---|---|---|---|---|
| 0.20 | 0.40 | 0.95 | 0.30 | 2.10 | 1.00 |
ALL WELD METAL MECHANICAL PROPERTIES (TYPICAL) :
| Hardness (HRC) |
|---|
| 36 - 40 (without treatment) |
RECOMMENDED WELDING CURRENT :
| Diameter (mm) | Current (A) |
|---|---|
| 3.15 | 90 - 120 |
| 4.00 | 150 - 180 |
| 5.00 | 190 - 230 |
Frequently Asked Questions
What is STAVITRODE A 57 used for?
STAVITRODE A 57 is an all purpose moly-manganese electrode for tough, hard and impact resistant surfacing of rail frogs and crosspieces, hammers, wobblers, excavators, pinions, couplings, tail bars, key ways, gear teeth, dozer sprockets, carrier and track rollers, idlers and crane wheels.
Can the STAVITRODE A 57 deposit be machined, and what is its hardness?
Yes, the weld metal is machinable. Its typical hardness is 36 - 40 HRC with no treatment.
Does STAVITRODE A 57 call for preheating or re-drying?
The preheat depends on the base material, and crack-sensitive materials need at least 300°C. Re-dry the electrodes for 1 hour at 100°C.
What amperage should I set for STAVITRODE A 57?
Set 90 - 120 A for 3.15 mm, 150 - 180 A for 4.00 mm and 190 - 230 A for 5.00 mm, on AC or DC (+).
STAVITRODE A 18
View details →
STAVITRODE A 46
View details →
STAVITRODE A 49
View details →
STAVITRODE A 58
View details →
STAVITRODE A 62
View details →
STAVITRODE A 71
View details →
STAVITRODE A 72
View details →
STAVITRODE A 74
View details →
STAVITRODE A 75
View details →
STAVITRODE A 79
View details →
STAVITRODE A 80(S)
View details →
STAVITRODE A 81
View details →Let’s find your welding solution.
Share your requirements. We’ll help you take the next step.