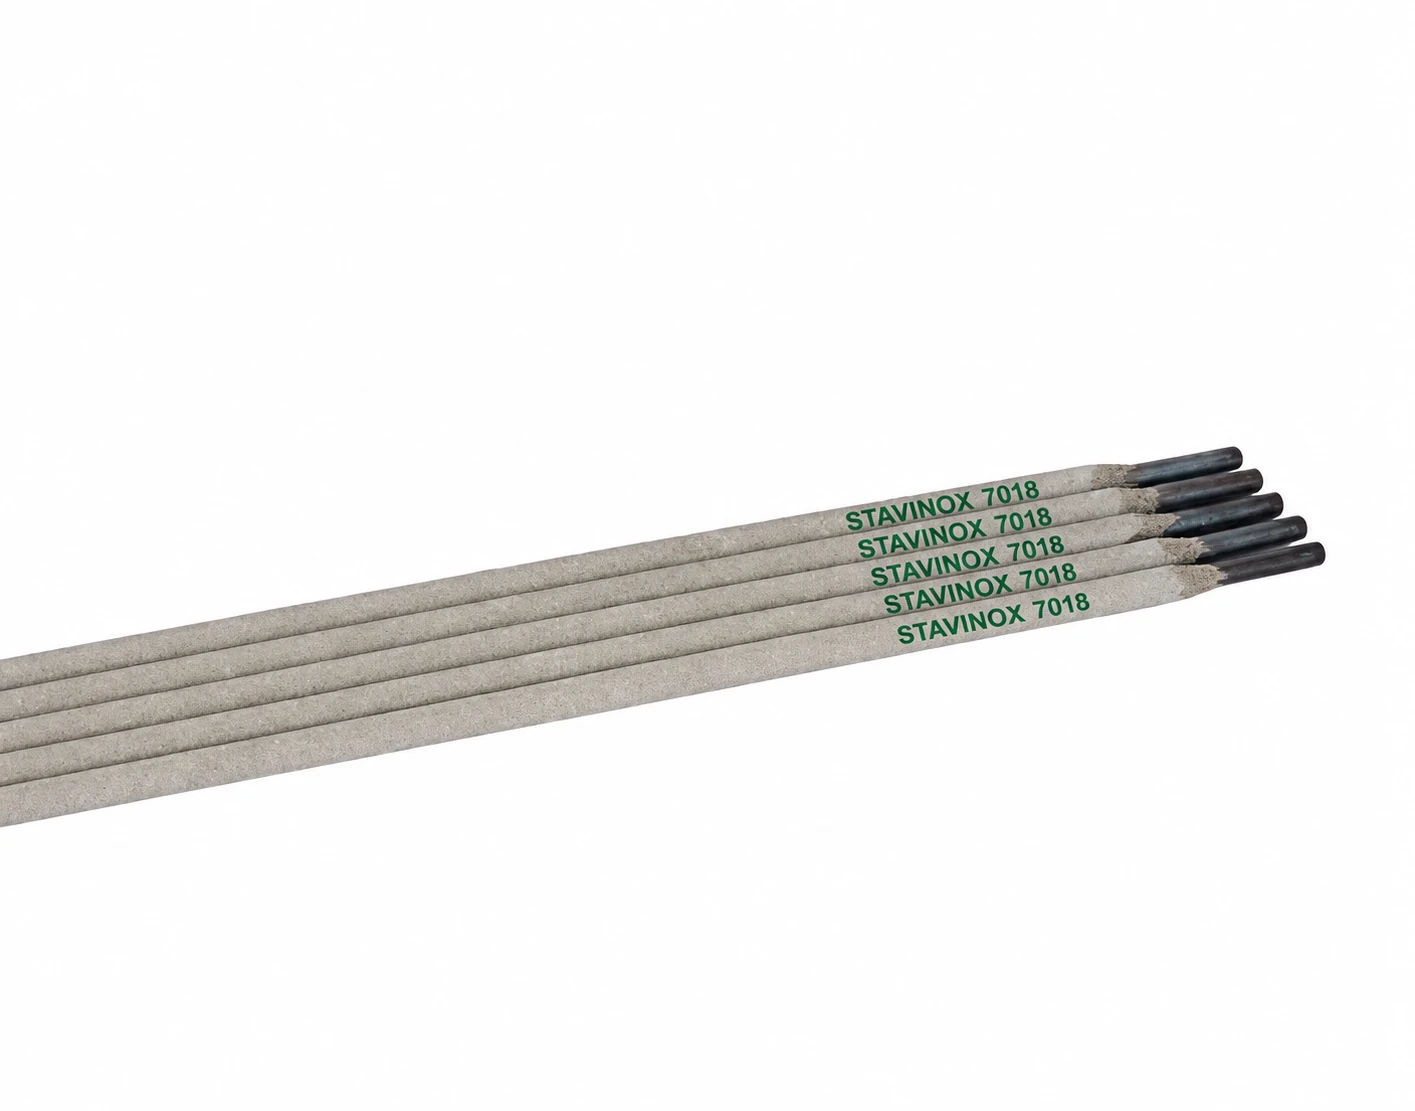
STAVINOX 7018
The 7018 welding rod, also called welding electrode 7018, is a premium low-hydrogen carbon steel electrode made for strong, durable and dependable welds. Its self-lifting slag leaves smooth, crack-free beads with very little spatter, so cleaning after welding is fast and simple. Very low diffusible hydrogen and excellent impact toughness lower the chance of hydrogen-induced cracking while delivering superior mechanical performance. STAVINOX 7018 suits structural steel, heavy machinery, pressure vessels and other critical applications, giving professional-grade welds in demanding industrial conditions.
Product details
Main Features and Benefits of the 7018 Welding Rod
The 7018 welding rod is a high-quality electrode that produces strong, dependable welds for industrial and structural work.
Simple Slag Removal
Self-lifting slag makes cleaning after welding quick and effortless, saving time and labour on every job.
Strength with Toughness
Gives excellent impact resistance and mechanical strength, for welds that are durable and long lasting.
Welds Free of Cracks
Reduces the risk of weld defects, so joints are safer and more dependable even under difficult conditions.
Even Weld Beads
Lays down neat, uniform beads and makes efficient use of material for high-quality results.
Low Hydrogen Level
Keeps hydrogen at an ultra-low level to avoid cracking and extend the life of the welded structure.
Flexible in Use
Works with both AC and DC(+) power sources, giving flexibility across different welding setups.
STAVINOX 7018 delivers dependable, efficient and high-quality welds, which is why professional welders prefer it.
7018 Welding Rod Technical Specifications
STAVINOX 7018 welding electrodes are built for strong, dependable welds and steady performance across many industrial applications.
|
Product Name |
AWS/SFA |
Yield Strength N/mm² |
Tensile Strength N/mm² |
Elongation A5 (%) |
Impact O V (J) |
Welding Conditions |
|
STAVINOX 7 |
E 7018 |
≥450 |
540–620 |
≥27 |
≥80 |
AC/DC(+) |
|
Stanvac 7018 |
E7018 |
≥450 |
550–620 |
≥28 |
≥80 |
DC(+) : AC |
|
STAVINOX 7018 |
E 7018-H4 |
≥450 |
550–620 |
≥28 |
≥90 |
AC; DC+ |
|
STAVINOX 7018(SP) |
E 7018-1 |
≥450 |
510–610 |
≥28 |
≥80 J at -50°C |
DC(+) ; AC |
|
STAVINOX 7018S |
E 7018-1 H4 |
≥450 |
550–620 |
≥28 |
80 J at -50°C |
- |
|
STAVINOX 7018SH4R |
E 7018-1 H4R |
≥450 |
550–640 |
≥28 |
80 J at -50°C |
- |
|
STAVINOX 7018H4R |
E 7018 H4R |
≥450 |
550–640 |
≥28 |
80 J at -40°C |
- |
|
STAVINOX 7018SW |
E7018 |
≥450 |
550–650 |
≥28 |
100 |
Together, these values mean our welding electrodes give strong, dependable welds with excellent mechanical performance in a range of applications and conditions.
Available 7018 Welding Rod Sizes
STAVINOX 7018 comes in the following welding rod and electrode sizes:
- 2.50 mm (3/32") - Intended for thin sections and root passes, at a lower amperage range.
- 3.15 mm (1/8") - The most popular 7018 size, used for general structural work.
- 4.00 mm (5/32") - The standard size for medium to heavy fabrication and fill passes.
- 5.00 mm (3/16") - For heavy-duty structural welding and high-deposition fill/cap passes.
All of these sizes are offered across all 8 product variants. Standard packs are 5 kg and 20 kg cartons, and 2 kg and 5 kg plastic tube packs are optional for smaller jobs.
7018 Welding Rod Characteristics
STAVINOX 7018 combines carefully engineered mechanical and chemical properties, so welds stay strong, durable and dependable across a broad range of applications.
Electrode Type
A low-hydrogen, iron-powder electrode built for a stable arc and consistent performance.
Compatible Materials
Well suited to carbon steel and low-alloy steel, so it fits many different welding projects.
Tensile Strength
High tensile strength produces solid joints that can carry heavy loads and structural stress.
Yield Strength
Stays stable and resists deformation under applied forces, protecting structural integrity.
Impact Toughness
Excellent notch impact resistance lets welds withstand static as well as dynamic loads.
Hydrogen Control
Ultra-low diffusible hydrogen (~4 ml/100 g weld metal) cuts the risk of hydrogen-induced cracking.
Weld Deposit Quality
Gives smooth, even beads with good fusion and few defects, for welds that last.
Deposition Efficiency
High deposition rates make efficient use of material, cut waste and raise productivity.
With these properties, STAVINOX 7018 is a dependable option for strong, durable and clean welds on all kinds of welding projects.
Related Products
Take a look at the other rod types in the STAVINOX range, each made for a particular welding need and for high-quality, dependable welds.
- STAVINOX 7018 (SP): A premium low-hydrogen electrode for critical structural and industrial welding.
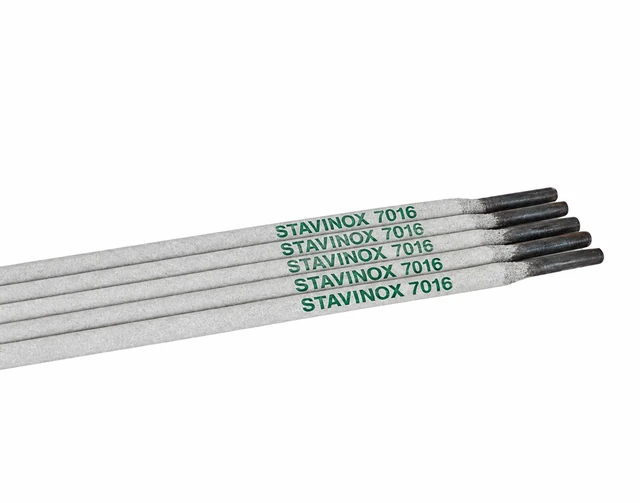
- STAVINOX 7016: Made for smooth weld beads, with excellent arc stability and less spatter.
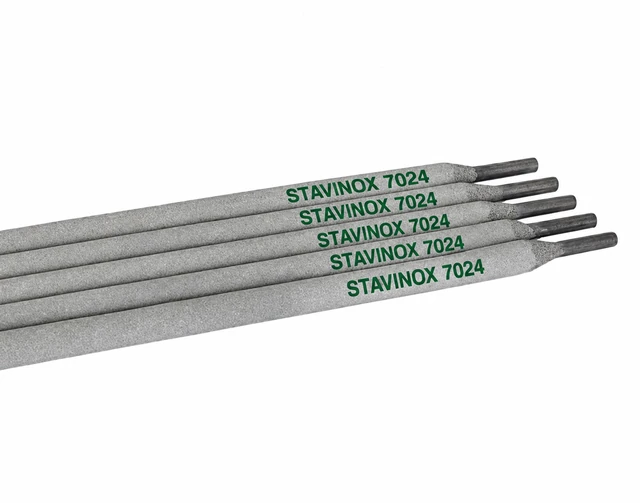
- STAVINOX 7024: A high-deposition electrode suited to heavy fabrication and large-scale projects.
- STAVINOX 6013: An easy-to-use electrode giving smooth welds and excellent all-position performance.
The STAVINOX electrodes form a full range of dependable, efficient welding solutions for varied applications and professional requirements.
Frequently Asked Questions
Which sizes does the 7018 welding rod come in?
STAVINOX 7018 is supplied in diameters of 2.50mm, 3.15mm, 4.00mm and 5.00mm. The 3.15mm (1/8") size is the one most often used for general structural welding, whereas 5.00mm is preferred for heavy fabrication and high-deposition work.
What are the standard electrode sizes for 7018?
Standard 7018 electrode sizes run from 2.50mm to 5.00mm, and each size matches a different plate thickness and amperage range. Small diameters (2.50mm) are used on root passes and thin sections, while large diameters (5.00mm) are used for fill and cap passes on thicker plate.
Is a 7018 welding rod suitable for cast iron?
A 7018 rod is not the best option for cast iron. Because 7018 is a carbon steel electrode, a nickel-based electrode such as STAVITRODE A-42 or STAVINOX CAST NiFe is recommended for cast iron. In an emergency field repair, 7018 can be used on cast iron with extensive preheating (250–300°C) and slow cooling, but the joint will not be machinable and may crack under thermal cycling.
How does 7018 differ from 7018-H4?
The 'H4' suffix tells you the electrode meets a tighter hydrogen limit: no more than 4 ml of diffusible hydrogen per 100g of deposited weld metal. Standard E7018 permits a higher hydrogen level. STAVINOX 7018 is classified as E7018-H4, which gives better crack resistance in critical structural applications.
Which rod types make up the 7018 family?
The 7018 family has 8 rod types: STAVINOX 7 (E7018), Stanvac 7018 (E7018), STAVINOX 7018 (E7018-H4), 7018(SP) (E7018-1), 7018S (E7018-1 H4), 7018SH4R (E7018-1 H4R), 7018H4R (E7018 H4R) and 7018SW (E7018). Each variant offers its own balance of strength, impact toughness and hydrogen control.
Which polarity is right for the 7018 welding rod?
Most 7018 variants run on DC positive (DC+), which gives deeper penetration. Several variants (STAVINOX 7018, 7018SP) can also be used with AC, so they work with both inverter and transformer machines. See the specifications table above for the exact welding conditions of each variant.
Let’s find your welding solution.
Share your requirements. We’ll help you take the next step.