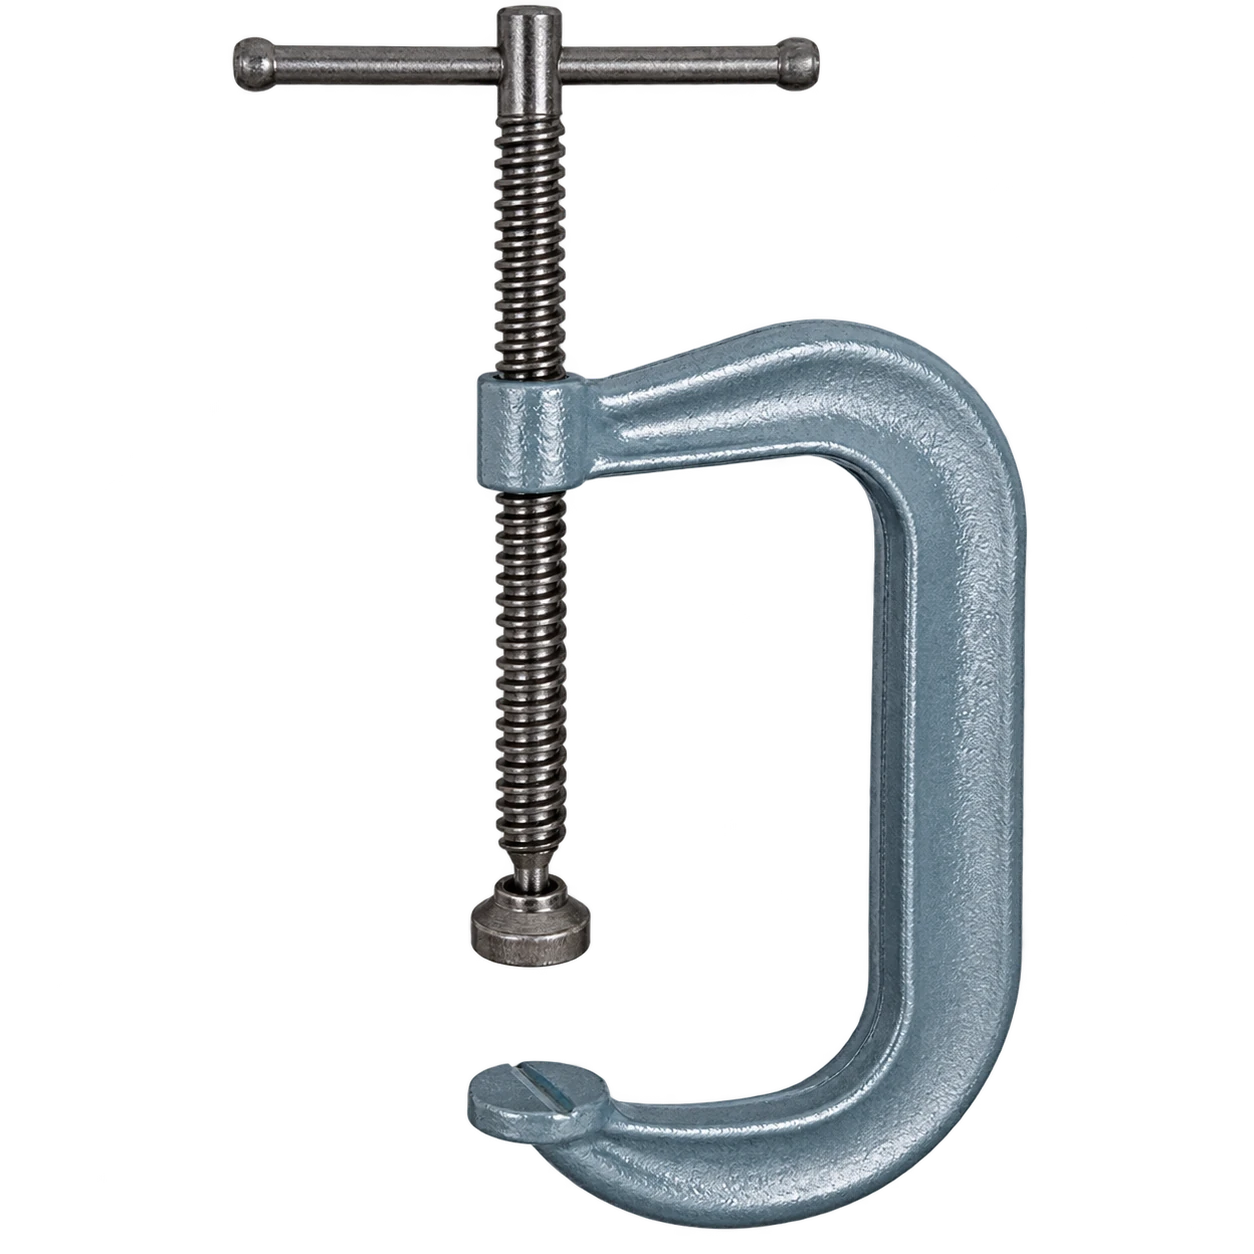
C-CLAMP
Stanvac International C-CLAMPS hold work firmly during fit-up, tacking and welding. Six sizes are offered from 0-2" up to 0-12", with throat depths from 2.25" to 6.30" and spindle diameters of 9/16", 3/4" and 7/8".
Product details
Key Features and Benefits of C-Clamp
- Six Sizes: From 0-2" up to 0-12" jaw capacity for light fit-up through to heavy assembly.
- Deep Throat: Throat depth from 2.25" to 6.30" reaches well in from the edge of the work.
- Heavy Spindle: Spindle diameters of 9/16", 3/4" and 7/8" give high clamping force.
- Drop-Forged Body: Rigid body resists spreading under load so the clamp holds its setting.
- Fabrication Ready: Suited to tack welding, fit-up, assembly and general workshop clamping.
Specifications of C-Clamp
The table below lists the models available in the C-Clamp range.
| Size | Throat Depth | Spindle Dia | Body Length |
|---|---|---|---|
| 0-2" | 2.25" | 9/16" | 5.2" |
| 0-4" | 3.25" | 3/4" | 8.0" |
| 0-6" | 4.0" | 3/4" | 10.6" |
| 0-8" | 5.0" | 3/4" | 13.0" |
| 0-10" | 6.0" | 3/4" | 15.3" |
| 0-12" | 6.30" | 7/8" | 18.3" |
Applications of C-Clamp
- Fabrication and welding workshops
- Construction and site erection work
- Plant maintenance and repair operations
- Training centres and tool rooms
Frequently Asked Questions
What is a welding C-clamp used for?
Holding fit-up during tacking and welding — pulling plate edges together, holding an angle against a face, clamping work to a table or fixture. In fabrication, the clamp is what makes the joint gap right before the welder commits to it.
What makes a welding C-clamp different from a general-purpose one?
Welding C-clamps are drop-forged for strength, built to take the heat near a weld without losing temper, and dimensioned for the reach and throat depth fabrication work needs. General-purpose clamps in cast iron crack under the load and heat that fabrication applies.
How do I choose the right size C-clamp?
Two dimensions matter. The opening is the maximum thickness it will span; the throat depth is how far in from the edge it can reach. Buyers usually check the opening and get caught by the throat — a clamp that opens wide enough but cannot reach the joint is no use. Size both against your typical work.
Can a C-clamp be used close to the weld?
Close, but not on the joint itself. Heat transmitted through the clamp softens the screw thread over repeated exposure and can distort a light clamp. Clamp far enough back that the work does not reach clamping temperature, and expect clamps used regularly near welding to have a shorter life.
How tight should a C-clamp be?
Tight enough to hold the fit-up without deforming the work. Overtightening bows thin sheet and pulls plate out of alignment, which produces a joint that fits under clamp and springs apart once released. If the clamp has to be strained to close the gap, the gap is a cutting or fitting problem, not a clamping one.
Should the earth be clamped to a C-clamp?
No. The earth return should go to the work or the table directly, through a proper earth clamp. Taking the return through a C-clamp puts welding current through a mechanical fastener with an uncontrolled contact area, which arcs at the screw thread and damages the clamp.
How should C-clamps be maintained?
Keep the screw thread clean and free of spatter, and wipe a light oil on it. Spatter welded into the thread is the commonest reason a clamp becomes stiff and eventually unusable. Anti-spatter spray on the threads before heavy work prevents most of it.
When should a C-clamp be taken out of service?
When the frame shows any crack, when the screw is bent, or when the swivel pad is missing or seized. A clamp that fails under load releases the work suddenly — on heavy section that is a serious hazard, so this is a scrap decision rather than a repair one.
Let’s find your welding solution.
Share your requirements. We’ll help you take the next step.