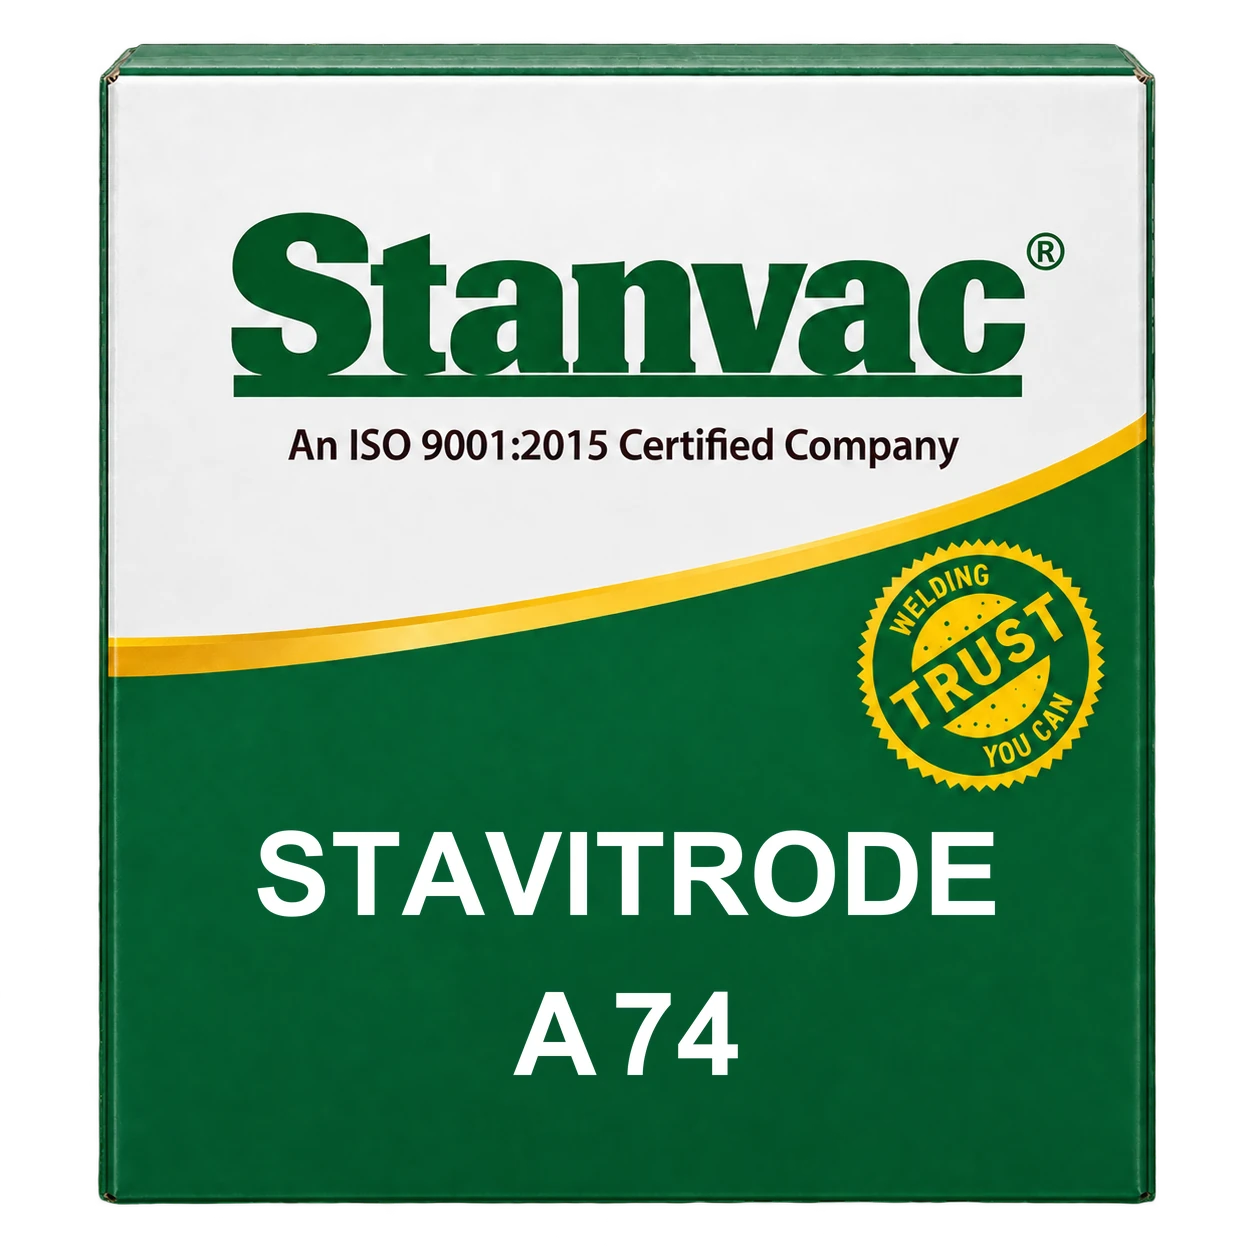
STAVITRODE A 74
DESCRIPTION & APPLICATIONS :
A basic coated hardfacing electrode usable in every position, for parts that suffer impact, compression and abrasive wear. It provides anti-wear protection on carbon steels and manganese steels.
Used for hardfacing and repairing ploughshares, crusher jaws, cutting tools, dipper teeth, bucket teeth and screw conveyors.
Welding technique: hold the electrode nearly vertical and keep the arc short; if required, re-dry for 2 hours at 300°C. Where the base is prone to cracking, put down a buffer layer of NiMnCr first. Low alloyed, high carbon tool steels need preheating anywhere from 200 - 400°C, depending on composition and thickness. After surfacing, let the part cool slowly in still air.
UNIQUE FEATURES :
- Resists wear, abrasion, impact and compression.
- Hardfacing in all positions, giving 60 - 63 HRC without treatment.
- The basic coating yields a tough deposit that resists cracks.
- Current: AC (50 V OCV) or DC (+).
Product details
KEY SPECIFICATIONS :
| C | Si | Mn | Cr | V | Mo | B |
|---|---|---|---|---|---|---|
| 0.50 | 1.00 | 1.00 | 8.50 | 1.80 | 1.50 | 0.20 |
ALL WELD METAL MECHANICAL PROPERTIES (TYPICAL) :
| Hardness (HRC) |
|---|
| 60 - 63 (without treatment) |
RECOMMENDED WELDING CURRENT :
| Diameter (mm) | Current (A) |
|---|---|
| 3.15 | 90 - 120 |
| 4.00 | 140 - 170 |
| 5.00 | 180 - 210 |
Frequently Asked Questions
What is STAVITRODE A 74 used for?
STAVITRODE A 74 is a basic coated, all position hardfacing electrode for anti-wear work on carbon and manganese steels, covering hardfacing and repair of screw conveyors, bucket teeth, dipper teeth, cutting tools, crusher jaws and ploughshares.
How hard is the STAVITRODE A 74 deposit?
Typically 60 - 63 HRC with no treatment, and it resists impact, compression and abrasive wear.
What preheat does STAVITRODE A 74 require?
A buffer layer of Ferrowork NiMnCr is recommended on crack-sensitive materials. Low alloyed, high carbon tool steels have to be preheated to 200 - 400°C depending on composition and thickness, and cooled slowly in still air after surfacing.
What amperage should I set for STAVITRODE A 74?
Set 90 - 120 A for 3.15 mm, 140 - 170 A for 4.00 mm and 180 - 210 A for 5.00 mm, on AC (50 V OCV) or DC (+). If necessary, re-dry at 300°C for 2 hours.
STAVITRODE A 18
View details →
STAVITRODE A 46
View details →
STAVITRODE A 49
View details →
STAVITRODE A 57
View details →
STAVITRODE A 58
View details →
STAVITRODE A 62
View details →
STAVITRODE A 71
View details →
STAVITRODE A 72
View details →
STAVITRODE A 75
View details →
STAVITRODE A 79
View details →
STAVITRODE A 80(S)
View details →
STAVITRODE A 81
View details →Let’s find your welding solution.
Share your requirements. We’ll help you take the next step.